Mafunso Ofunsidwa Kawirikawiri (FAQ)
To assist technical buyers and supply chain directors in evaluating automation strategies, here are answers to common questions regarding the implementation of an AS/RS in chemical industry applications:
Q1: How does an AS/RS handle hazardous or volatile chemical storage safely?
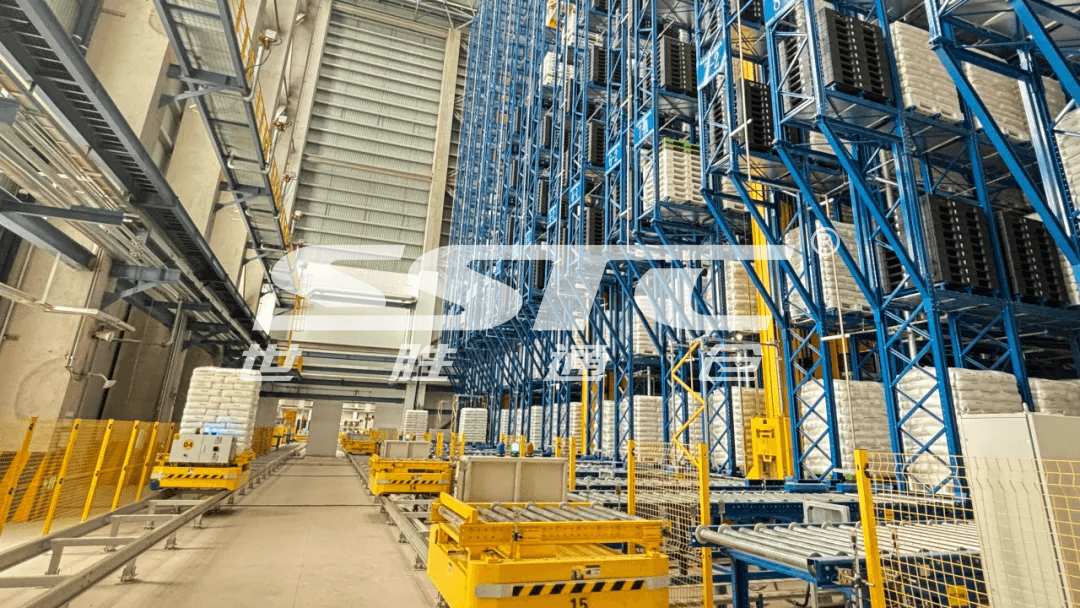
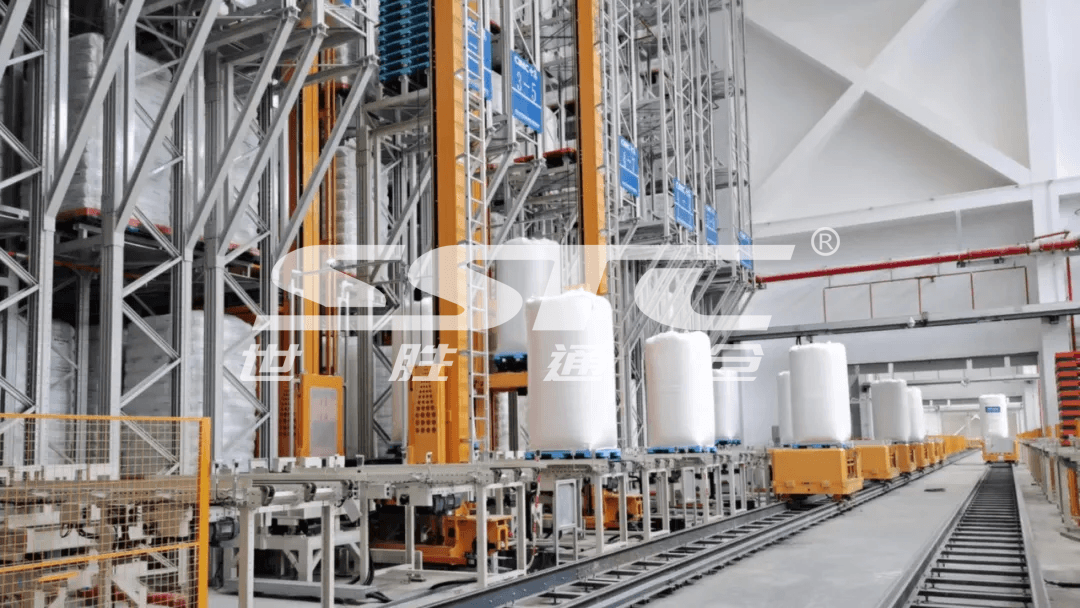
A: An AS/RS removes human operators entirely from high-bay storage zones through unmanned stacker cranes and automated conveyors. Komanso, systems can be customized with explosion-proof (Ex-rated) electrical components, corrosion-resistant coatings, and specialized fire-suppression interface protocols to ensure complete safety when handling volatile substances.
Q2: What is the maximum height and load capacity of an AS/RS engineered by SSTC Intelligence?
A: SSTC Intelligence high-bay AS/RS solutions can be engineered to heights exceeding 25 mita, with stacker crane unit-load capacities designed to handle heavy industrial pallet weights ranging from 1,000 kg to over 2,500 kg per storage position.
Q3: How does AS/RS integrate with our existing enterprise software (ERP)?
A: The AS/RS is controlled via an advanced Warehouse Control System (WCS) and Warehouse Management System (WMS) that features standard API and middleware gateways, allowing seamless, real-time data synchronization with enterprise ERP platforms like SAP, Oracle, and Microsoft Dynamics.
Q4: Can an AS/RS be retrofitted into an existing chemical manufacturing facility?
A: Yes. While greenfield installations offer maximum layout freedom, SSTC Intelligence specializes in brownfield retrofits, adapting high-bay AS/RS architecture to integrate with existing building envelopes and production line layouts.
Conclusion: Future-Proofing Your Chemical Supply Chain
As global chemical markets grow increasingly competitive and regulatory frameworks tighten, supply chain resilience, absolute safety, and spatial optimization are non-negotiable prerequisites for corporate survival. Transitioning from legacy manual storage to an intelligent, automated infrastructure allows chemical enterprises to protect their workforce, eliminate storage bottlenecks, and scale operations seamlessly.
Zithunzi za STTC Intelligence delivers world-class, turnkey AS/RS solutions tailored to the rigorous demands of the chemical industry. Whether you are planning a high-bay warehouse retrofit or designing a new automated facility, our engineering team is ready to help you optimize your infrastructure.
To explore how our custom automated solutions can transform your facility, visit our official website at www.sstc-storage.com.