The Professional Manufacturing Supplier of High Density Storage Solutions in China


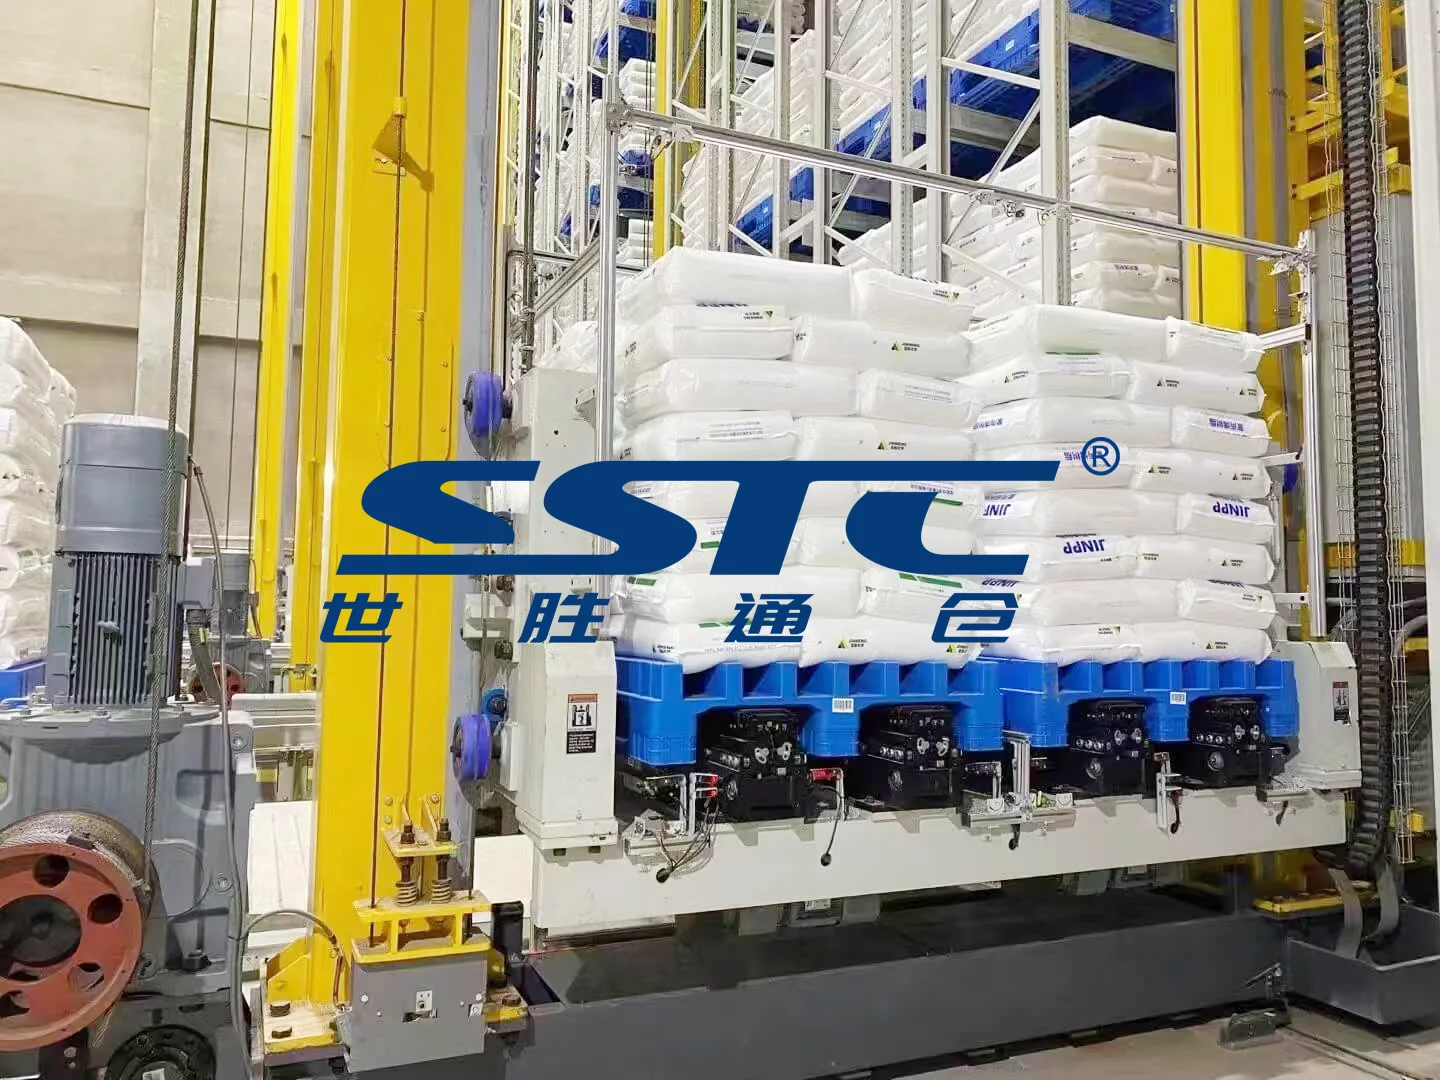
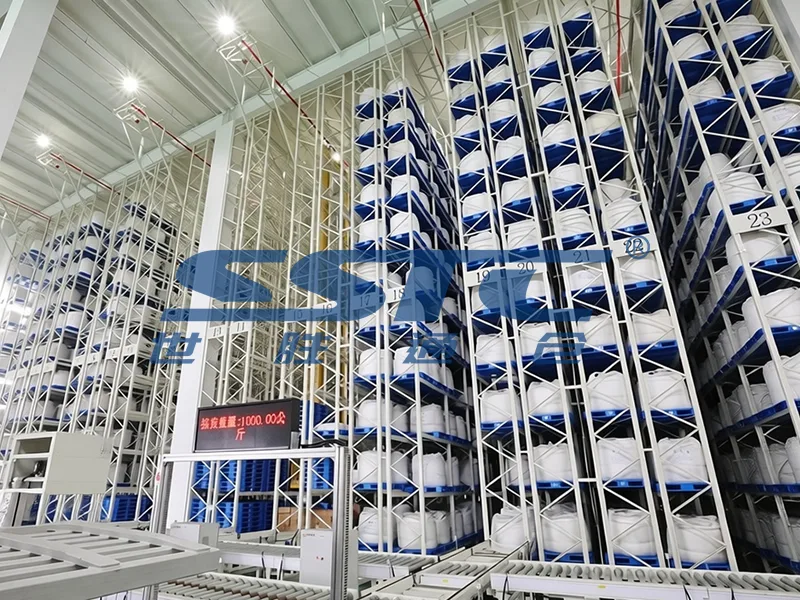
| SSTC automated storage and retrieval system operating in a modern chemical and advanced materials storage facility中文/CN

Pallet AS/RS Solutions For Chemical Warehouse Automation

How Does Pallet AS/RS Transform Safety and High-Density Storage in Chemical Warehousing?

Deploying Pallet AS/RS with dual-station double-deep stacker crane technology expands vertical cubic storage density by up to 200% in modern chemical manufacturing and distribution facilities, eliminating high-hazard forklift traffic and guaranteeing 100% batch traceability. As global chemical supply chains adapt to stringent safety directives highlighted in industrial logistics coverage by Chemical Engineering Magazine, chemical producers face rising pressures to optimize storage footprints while strictly adhering to hazardous material containment standards. Storing heavy raw materials, resins, polymer granules, and specialty chemical containers requires high-capacity, touchless automated infrastructure engineered specifically for corrosive or hazardous industrial environments.

Implementing customized chemical industry storage solutions engineered by SSTC Intelligence enables plant operators to transform volatile floor space into high-density automated storage ecosystems. Operating dual-station double-deep stacker cranes allows automated systems to handle two pallets simultaneously across deep-lane racking channels, doubling throughput efficiency during peak load cycles. By removing manual forklift operators from dangerous storage aisles and replacing traditional rack layouts with factory-direct automated high-bay infrastructure, chemical manufacturers achieve total inventory control, mitigate operational risks, and maintain compliance from raw chemical receiving to final export dispatch.

High-bay Pallet AS/RS operating dual-station double-deep stacker crane system handling two heavy chemical material pallets simultaneously inside climate-controlled automated warehouse engineered by SSTC Intelligence

What Critical Operational Vulnerabilities Impact Traditional Chemical Storage?

Chemical processing and material distribution hubs navigate strict environmental safety compliance, heavy unit payloads, and intense order fulfillment velocity. Storing bulk raw polymers, specialty liquid totes, and hazardous chemical drums using standard forklifts creates distinct operational liabilities:

High Weight Payloads & Floor Damage

Chemical containers typically exceed 1,200 kg to 1,500 kg per pallet. Conventional floor stacking leads to bottom-tier structural fatigue, floor slab cracking, and hazardous spill risks caused by uneven stack lean.

Operator Safety & Spill Risks

Operating manual forklift trucks inside narrow aisles with hazardous materials increases collision exposure. Human error during high-reach maneuvers can puncture chemical drums or spill corrosive liquids, forcing costly facility shutdowns.

Complex Quarantine & Expiration Audits

Specialty resin additives and reactive chemical compounds require strict batch isolation and precise FIFO/FEFO tracking. Paper-based or manual WMS logging leads to batch mixing and regulatory non-compliance during safety audits.

Engineering research published in the Journal of Loss Prevention in the Process Industries emphasizes that automated material isolation and touchless transfer systems cut chemical handling incidents by over 85%. Transitioning to high-bay automated racking removes human operators from high-risk storage zones, establishing absolute operational containment.

How Do Dual-Station Double-Deep Stacker Cranes Maximize Chemical Throughput?

Engineered to resolve extreme spatial constraints and demanding inbound/outbound schedules in chemical logistics, SSTC Intelligence delivers custom high-bay automated infrastructure. Integrating dual-station double-deep stacker cranes converts standard chemical warehousing into high-performance, automated material handling hubs.

Dual-Station Simultaneous Handling in Pallet AS/RS

Equipping Pallet AS/RS with dual-station stacker crane carriages enables simultaneous pickup, transport, and placement of two independent chemical pallets per travel cycle. This configuration doubles total hourly movement velocity compared to conventional single-station cranes, drastically reducing truck staging wait times during peak chemical raw material arrivals.

Volumetric Density Expansion via Double-Deep Pallet AS/RS

Deploying specialized Double-Deep Pallet AS/RS racking structures allows chemical facilities to store pallets two deep within each storage channel. By eliminating nearly 50% of inner aisle requirements across heights reaching 30 meters, plant operators maximize storage density while maintaining heavy payload support up to 1,500 kg per bay.

Hazardous Environment Compliance: Engineering Anti-Explosive and Heavy Steel Racking

Operating inside chemical production environments demands strict compliance with international hazardous containment standards. Storing flammable solvents, polymer additives, and volatile chemical reagents requires specialised infrastructure capable of preventing ignition sources and resisting corrosive atmospheric degradation.

To meet these stringent criteria, SSTC Intelligence incorporates ATEX-certified explosion-proof servo motors, non-sparking polyurethane guide wheels, and anti-static grounding systems across every custom AS/RS Stacker Crane System. Electrical enclosures feature positive-pressure purge systems to eliminate hazardous vapor ingress entirely.

Additionally, high-bay racking frameworks utilize high-grade structural steel treated with hot-dip galvanization or specialized epoxy powder coatings. This heavy-duty engineering protects structural integrity against corrosive chemical vapors while sustaining continuous, heavy pallet loads up to 1,500 kg per storage position across extreme vertical heights.
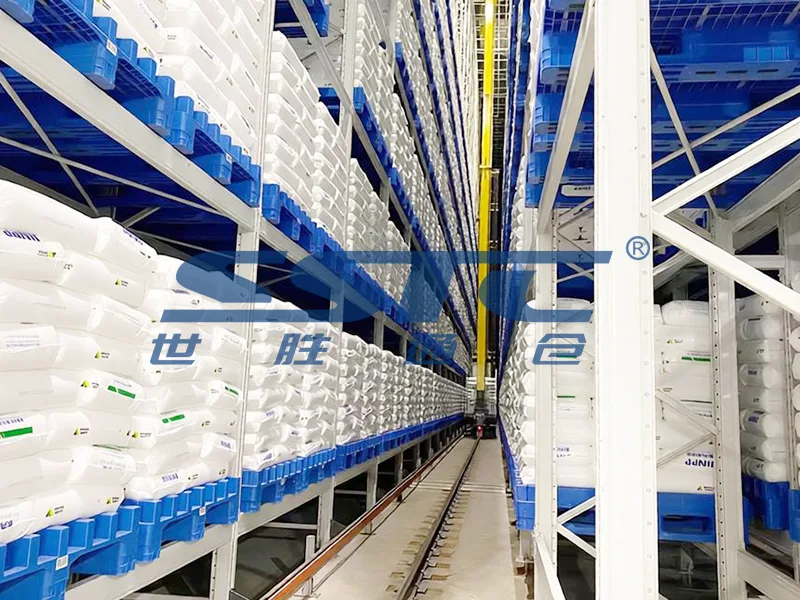
Heavy-duty high-bay steel racking frame within Pallet AS/RS storing heavy resin drums and chemical totes engineered by SSTC Intelligence

Intelligent Inbound Inspection and WES Batch Control Systems

Precision material handling begins before a chemical pallet enters the racking aisle. Before transfer to high-bay storage channels, inbound loads pass through automated sizing gates equipped with photoelectric sensor arrays, laser profile scanners, and integrated weight scales to detect damaged skids or overhang risks.

SSTC Intelligence embeds custom Warehouse Execution System (WES) software platforms that orchestrate real-time movement across the entire Pallet AS/RS footprint. The software dynamically interfaces with corporate ERP systems to enforce strict First-In, First-Out (FIFO) and First-Expired, First-Out (FEFO) picking algorithms required for reactive chemical compounds.

By connecting automated roller conveyors directly to Double-Deep Pallet AS/RS stacker crane pick points, chemical processing plants eliminate bottlenecks during raw material receiving. Automated tracking guarantees 100% batch traceability, preventing dangerous inventory mix-ups and streamlining regulatory compliance audits.
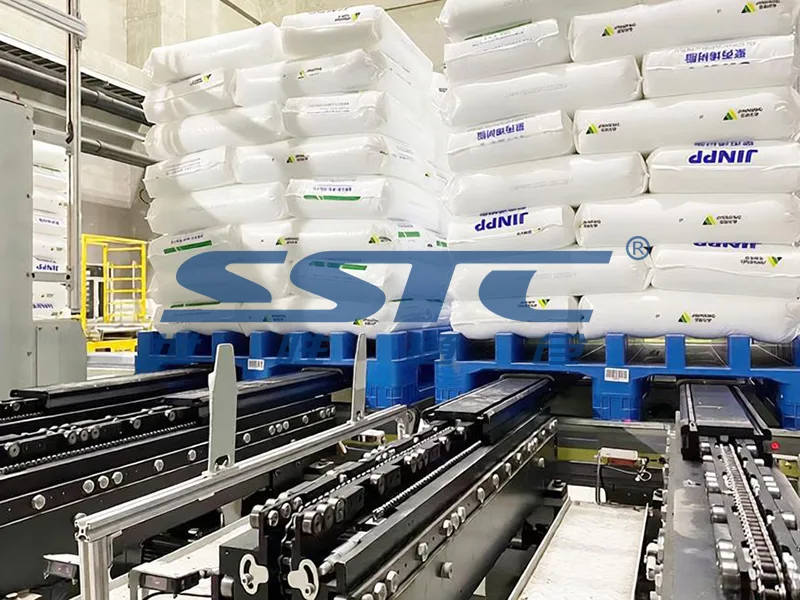
Heavy-duty automated roller conveyor line transferring chemical material pallets into high-bay Pallet AS/RS staging area engineered by SSTC Intelligence

Real-Time WES Dashboard: 100% Chemical Batch Isolation and Traceability

Managing volatile chemical inventories requires rigorous quarantine enforcement and immediate batch locking capability. SSTC Intelligence customizes WES software interfaces to provide plant managers with real-time visual monitoring across every high-bay storage cell.

When raw material batches undergo quality control or safety inspections, software algorithms instantly isolate designated pallet positions within Double-Deep Pallet AS/RS racking channels, preventing unauthorized retrieval cycles automatically.

System dashboards track expiration timelines for temperature-sensitive liquid additives, automatically prioritizing FEFO picking queues. Touchscreen terminals mounted inside hazardous control hubs ensure seamless operator oversight while keeping human personnel safely outside automated high-bay crane aisles.
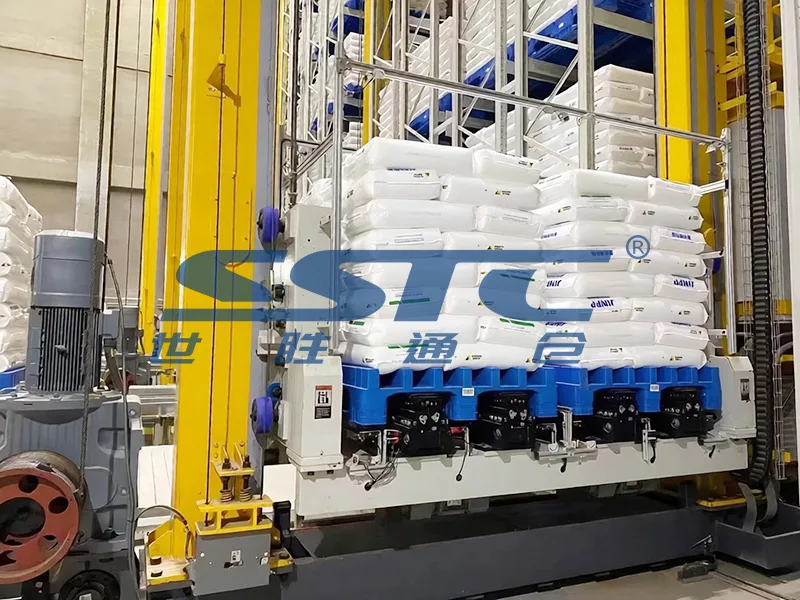
Real-time WES warehouse execution system dashboard managing inventory accuracy and chemical batch traceability within Pallet AS/RS engineered by SSTC Intelligence

EN ISO Compliant Safety Perimeter Fencing and Hazard Containment
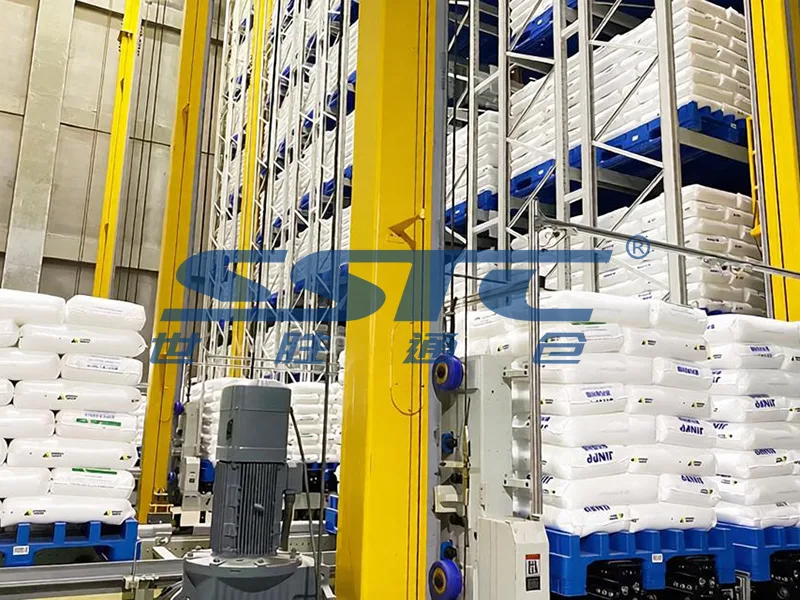
EN ISO safety perimeter fencing and optical light curtains securing automated AS/RS stacker crane operation zone engineered by SSTC Intelligence

Protecting facility personnel from high-speed automated equipment requires physical and optical containment barriers. High-bay AS/RS Stacker Crane System corridors operate behind full-height perimeter steel safety mesh engineered according to EN ISO 14120 standards.

Access points integrate safety-interlocked access gates and multi-beam safety light curtains. If personnel breach active travel zones during emergency maintenance, photoelectric sensing relays trigger instant safety stops, halting stacker crane travel within milliseconds.

This zero-compromise safety architecture prevents unauthorized human access into active high-bay aisles while ensuring fully compliant operation in chemical plants handling hazardous drum loads and polymer containers.

Climate-Controlled Automated High-Bay Racking for Sensitive Polymers

Specialty resin compounds, reactive chemical catalysts, and raw polymer granulates frequently require strict climate-controlled environments to prevent moisture absorption, thermal degradation, or premature curing.

SSTC Intelligence customizes Pallet AS/RS infrastructure specifically for regulated thermal zones ranging from +5°C temperature-controlled chambers to specialized low-humidity storage bays. Mechanical components feature low-temperature synthetic lubricants and moisture-sealed IP65 sensor enclosures.

Optimized vertical airflow channels within heavy-duty racking frames maintain uniform temperature distribution across all vertical storage levels, protecting high-value chemical raw materials against degradation throughout long-term buffer storage.
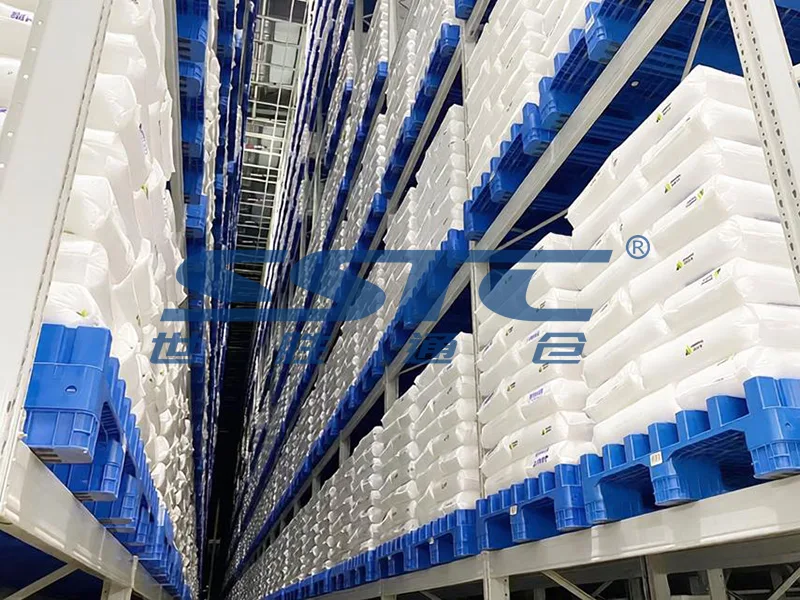
Climate-controlled temperature-regulated automated storage zone inside chemical Pallet AS/RS facility engineered by SSTC Intelligence

Rapid Outbound Dispatch Staging and Turnkey Engineering Solutions
High-speed outbound dispatch staging conveyor and automated stretch wrapping station linked with Double-Deep Pallet AS/RS engineered by SSTC Intelligence

Outbound logistics velocity directly dictates chemical production plant efficiency. Automated high-bay retrieval cycles feed finished chemical pallets directly onto high-speed discharge roller loops integrated with automated stretch wrappers.

By securing pallet loads before truck staging, Double-Deep Pallet AS/RS prevents pallet instability during transit. Automated staging lanes buffer ready-to-ship orders, allowing forklift operators to complete container loading in under 15 minutes per trailer.

Partnering with SSTC Intelligence ensures factory-direct turnkey engineering—from preliminary 3D simulation drafting to structural racking fabrication, on-site stacker crane commissioning, and lifetime WES software support.

Upgrade Your Chemical Facility with Customized Pallet AS/RS Engineering

Contact the senior warehouse automation engineering team at SSTC Intelligence to evaluate your chemical facility floorplan, calculate double-deep storage ROI, and design custom explosion-proof high-bay racking systems.

Explore Chemical Application Case Studies

Future Industry Demand: Projected Growth for Automated Chemical Logistics

Accelerating global demand for specialty resins, fine chemicals, and advanced battery materials is forcing chemical manufacturing enterprises to modernize legacy storage operations. Market research highlights a decisive global shift toward high-density automated material handling infrastructure tailored for hazardous materials:

$412.8 Billion

Global Chemical Logistics Expansion by 2032

According to research from Precedence Research, the global chemical logistics market is projected to grow from $275.4 billion to $412.8 billion by 2032, driven by strict hazardous material safety regulations and high-volume raw material throughput.

Source: Precedence Research - Chemical Logistics Market Size & Forecast Report.

7.3% CAGR

Accelerating Demand for High-Bay AS/RS Systems

Industry analysis by Grand View Research confirms that the global AS/RS market is expanding at a 7.3% CAGR through 2030, with chemical processing plants accounting for the fastest growth sector due to urgent floor space optimization and workforce safety mandates.

Source: Grand View Research - Automated Storage & Retrieval System Industry Analysis.

To capitalize on these expansion trends, forward-thinking chemical plants are replacing manual forklift bays with high-bay Pallet AS/RS infrastructure, securing long-term operational scalability, regulatory safety compliance, and maximum land utilization.

Frequently Asked Questions About Chemical Industry Automation

Q How does Pallet AS/RS handle corrosive chemical vapors and hazardous materials?
A SSTC Intelligence engineers Pallet AS/RS infrastructure with ATEX explosion-proof motors, anti-corrosive hot-dip galvanized structural steel, and positive-pressure purge electrical enclosures to guarantee absolute safety and material containment in volatile chemical facilities.
Q What is the throughput advantage of dual-station stacker cranes in chemical plants?
A Equipping an AS/RS Stacker Crane System with dual-station carriages enables the simultaneous handling of two independent chemical pallets per travel cycle, doubling hourly throughput velocity and eliminating truck staging bottlenecks during peak raw material arrivals.
Q How does WES software ensure batch traceability and safety compliance?
A Custom WES software platforms integrate directly with corporate ERP systems to enforce strict FIFO and FEFO picking protocols, empowering plant managers to execute instant batch quarantine and maintain 100% traceability across all Double-Deep Pallet AS/RS storage channels.
Q What is the typical installation timeframe for chemical warehouse automation?
A A high-bay Pallet AS/RS facility with 5,000 to 10,000 pallet positions typically requires 120 to 150 days from preliminary structural steel erection to full WES software commissioning, managed through turnkey on-site engineering by SSTC Intelligence.

Transform Your Chemical Supply Chain with SSTC Intelligence

As chemical manufacturing plants face increasing pressures to maximize vertical storage capacity and eliminate hazardous manual touchpoints, investing in factory-direct automated storage solutions is essential for sustainable growth. Partner with SSTC Intelligence to engineer custom, explosion-proof automated high-bay systems tailored precisely to your facility requirements.

Explore Chemical Application Case Studies

Connect with SSTC Intelligence Warehouse Engineering Specialists

Global Sales & Engineering Headquarters

Consult directly with senior automation engineers to design high-bay Pallet AS/RS racking structures, evaluate hazardous chemical containment requirements, or request customized 3D layout proposals.

Request Technical Consultation

Turnkey Project Inquiries & Quotations

SSTC Intelligence provides factory-direct manufacturing, international logistics dispatch, on-site mechanical erection, and lifetime WES software support for global chemical logistics projects.

  • Email Consultation: [email protected]
  • Service Scope: Worldwide Installation & Commissioning
  • Compliance Standards: EN ISO, FEM, & GB Structural Compliance

Strategic Engineering Brief: Why Dual-Service Stacker Crane AS/RS Is Redefining Chemical Supply Chain Resilience by SSTC Intelligence Technology

Prev:

Next:

Leave a message