
 SSTC Intelligence High Density AS/RS Storage Systems
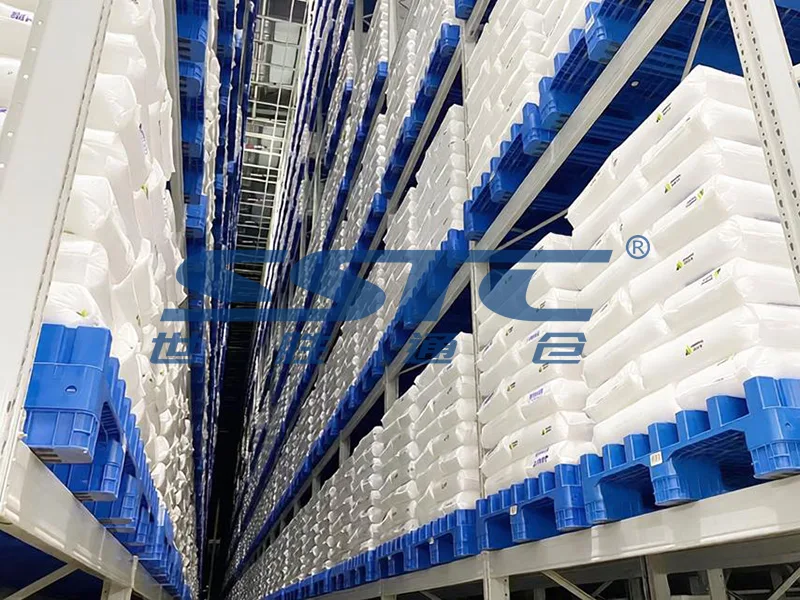
Engineering Dual-Station Double-Deep Stacker Cranes
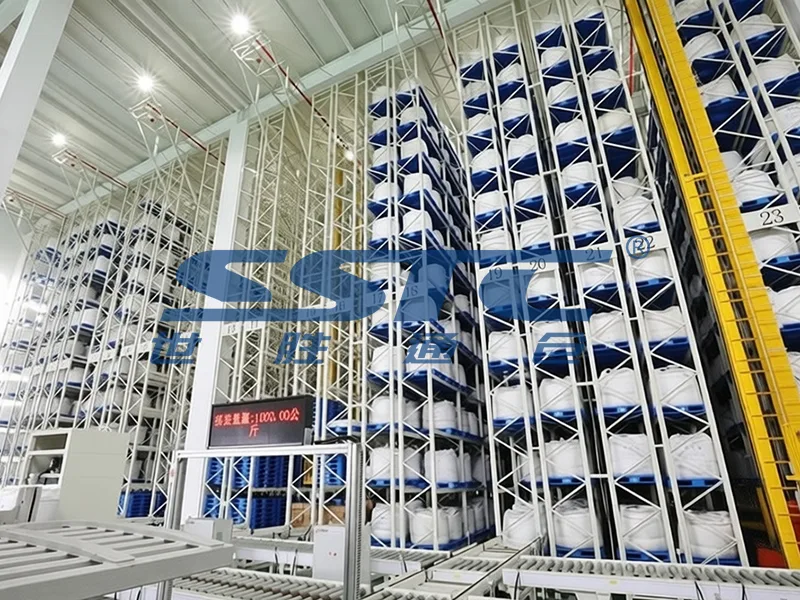
Achieving extreme storage density without sacrificing cycle speed requires structural innovation. Traditional single-pallet stacker cranes create operational bottlenecks during high-volume raw material feeding. SSTC Intelligence solves this by pairing high-bay Double-Deep Pallet AS/RS racking with specialized dual-station carriages.
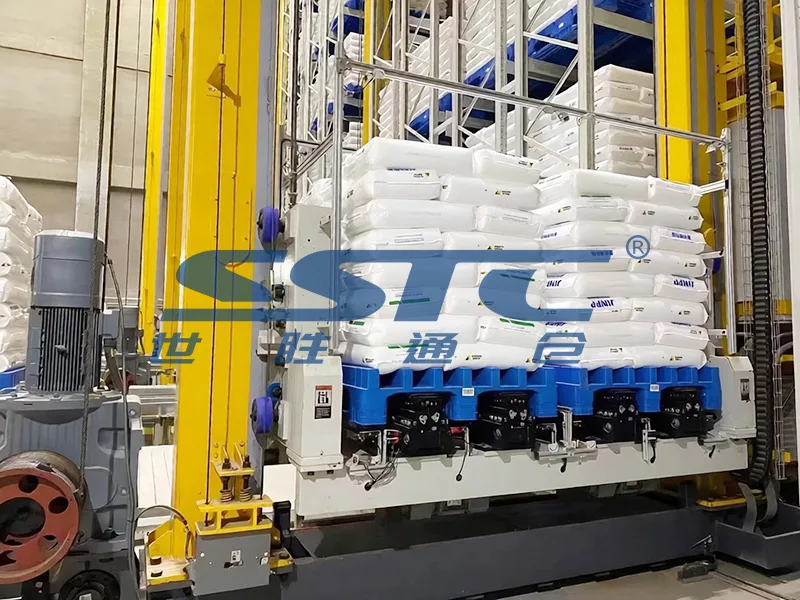
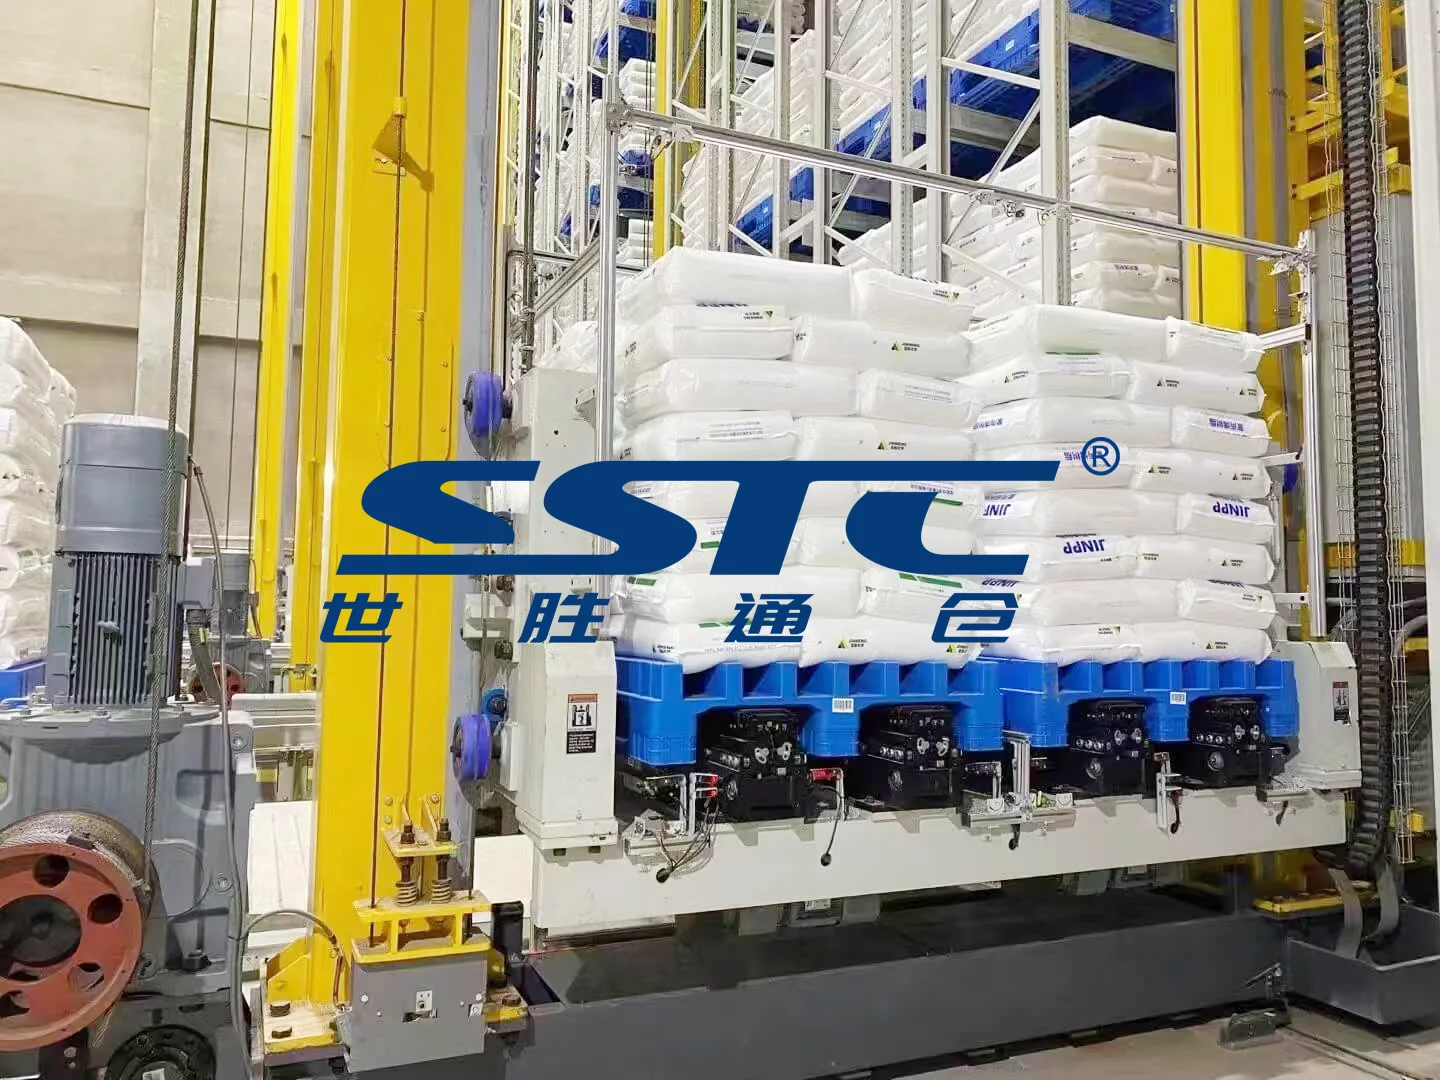
Dual-Station Synchronous Pallet Handling Action
The dual-station carriage picks or deposits two chemical pallets simultaneously, doubling hourly transport velocity across high-bay storage lanes during peak material movements.
High-Throughput Engineering Performance Benchmarks
Deploying an advanced AS/RS Stacker Crane System inside chemical storage offers distinct operational performance advantages:
- Double Storage Density: Double-deep telescopic forks eliminate half the operating aisles, boosting footprint utilization.
- 200% Velocity Increase: Simultaneous dual-pallet movements double inbound raw material processing speeds.
- Zero Handling Damage: Automated laser positioning prevents fork impacts on sensitive chemical containers.
- 100% WES Integration: Real-time synchronization prevents inventory bottlenecks and ensures dynamic aisle load balancing.
- 24/7 Continuous Efficiency: Regenerative power braking reduces energy consumption during heavy pallet lowering cycles.
By upgrading to dual-station technology, chemical producers achieve maximum pallet capacity per square meter while keeping pace with rapid continuous production demands.
Industrial Safety & Anti-Corrosion Engineering
Chemical logistics environments present aggressive operating conditions, including corrosive vapors, volatile organic compounds, and heavy pallet floor loads. Standard commercial warehousing equipment degrades rapidly under these factors. Successful implementations documented in our chemical case studies demonstrate how custom material selection and active safety containment prevent costly operational downtime.
Comprehensive Chemical Warehouse Safety Protocols
Engineering specialized Chemical Warehouse Automation requires strict adherence to international safety and explosion protection standards:
- ATEX Explosion-Proof Drives: Sealed explosion-proof motors and spark-resistant wheels eliminate ignition hazards in hazardous storage zones.
- EN ISO Safety Enclosures: Physical perimeter fencing with interlocking access gates prevents unauthorized human entry into operating crane aisles.
- Active Chemical Containment: Integrated spill catch basins under racking uprights contain accidental drum or tote leaks immediately.
- Positive-Pressure Panels: Purged electrical cabinets prevent corrosive ambient gases from damaging delicate drive electronics.
- Optical Light Curtains: Instant emergency braking activates if personnel cross perimeter safety boundaries during automated operations.
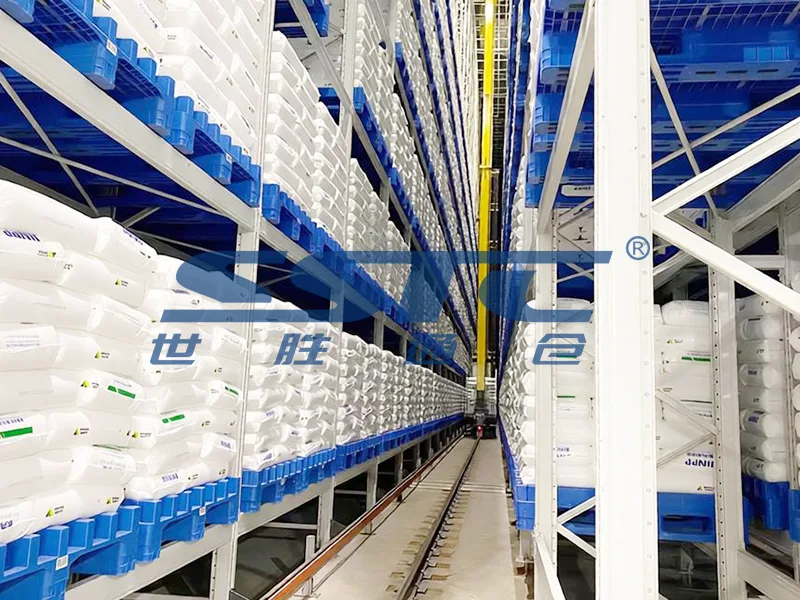
Heavy-Duty Corrosion-Resistant Racking Framework
High-bay structural steel uprights treated with industrial epoxy or hot-dip galvanizing withstand harsh chemical vapors while maintaining structural integrity under 1,500 kg pallet loads.
Combining heavy-duty mechanical anti-corrosion treatments with intelligent safety sensing ensures total compliance with international industrial safety mandates while protecting long-term capital investments.
WES Software Intelligence & Chemical Batch Traceability
Physical high-density storage hardware requires advanced digital control to manage sensitive chemical raw materials safely. Integrating intelligent Warehouse Execution Systems (WES) transforms automated storage into a fully transparent node within supply chain networks, ensuring strict compliance and zero inventory blind spots.
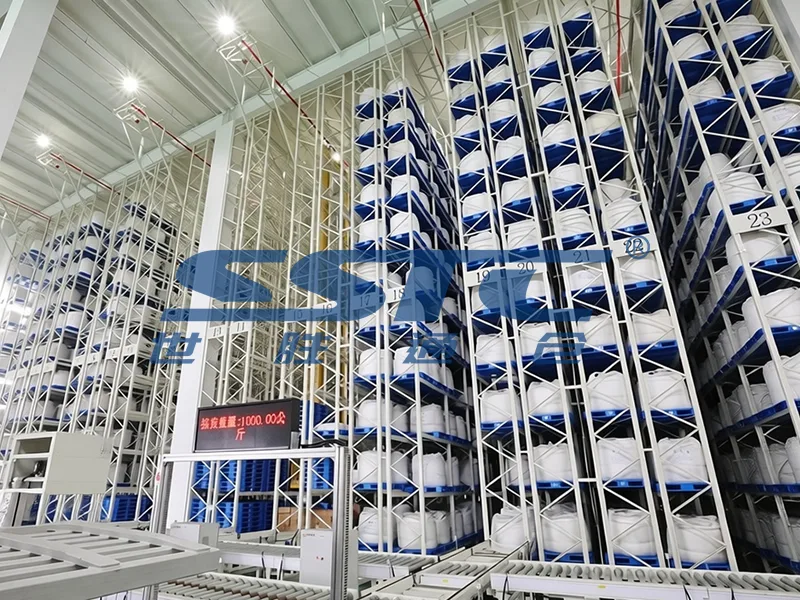
Automated Inbound Conveyor Processing Station
Heavy-duty roller conveyor lines scan, weigh, and profile incoming chemical pallets automatically, registering lot data seamlessly into the WES system before crane pickup.
Digital Traceability & Smart Inventory Control
Deploying advanced WES Software solutions guarantees absolute precision across complex chemical workflows:
- Strict FIFO/FEFO Rotation: Automated algorithms prioritize older chemical batches to prevent product degradation and expiration.
- 100% Chemical Batch Traceability: Instant scan-to-source tracking links raw material lot numbers directly to outgoing finished product containers.
- Dynamic Slotting Optimization: High-turnover chemical skids are automatically assigned to optimal lower rack levels for faster crane retrieval.
- Error-Proofing Barcode Validation: Automated scanner checks verify pallet barcodes against ERP orders before allowing crane placement.
- Automated Exception Alerts: Immediate system notifications flag weight discrepancies, temperature spikes, or obstructed storage lanes.
By pairing high-performance stacker crane mechanics with intelligent Chemical Batch Traceability software, chemical manufacturers achieve total operational excellence, minimizing error rates while accelerating fulfillment speed.