
 SSTC Intelligence High Density AS/RS Storage Systems
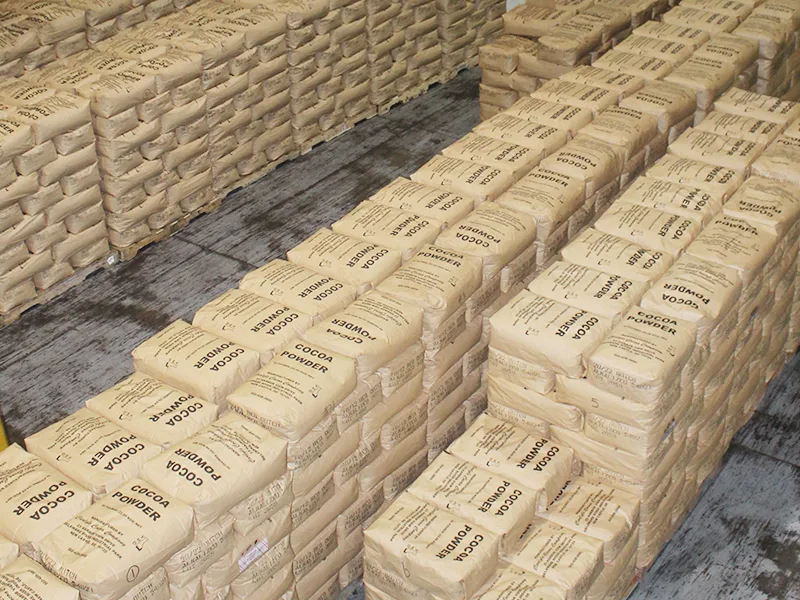
Deploying Pallet AS/RS expands vertical cubic storage density by up to 180% in Malaysian cocoa processing facilities, eliminating raw material staging bottlenecks and guaranteeing 100% FEFO dispatch compliance. As Malaysia reinforces its reputation as the leading cocoa grinding and export hub across the Asia-Pacific region, processing plants located near key maritime hubs in Johor and Klang face severe warehouse spatial constraints. Managing high-frequency throughput across standardized pallets of raw cocoa beans, packaging supplies, and heat-sensitive cocoa butter requires dense, touchless material handling infrastructure engineered specifically for tropical operating environments.
Industrial performance reports published by the Malaysian Cocoa Board (LKM) emphasize that Malaysia accounts for a major share of global cocoa butter and powder production. However, handling heavy cocoa derivative loads on standardized pallets using traditional floor stacking or conventional forklift trucks introduces widespread double-handling, pallet damage, and cooling energy waste. By transitioning static floor space into automated high-bay racking engineered by SSTC Intelligence, refinery operators unlock immediate operational throughput while protecting product quality from factory floors to export containers.
What Are the Primary Storage Pain Points in Malaysian Cocoa Processing?
Cocoa processing plants operate under stringent food safety, environmental, and inventory control constraints. Raw cocoa beans arrive in bulk or standardized bags on pallets, while refined cocoa butter, cocoa liquor blocks, and alkalized cocoa powder are packaged into standardized industrial units. The primary logistics challenges include:
Multi-SKU High-Frequency Rotation
Processing facilities must balance hundreds of distinct SKUs, ranging from raw bean origins to customized butter formulations. Manual forklift handling often results in double-handling errors, product damage, and delayed export staging.
Land & Spatial Footprint Limits
Industrial land around major port corridors in Johor and Selangor carries premium acquisition costs. Traditional single-deep racking or floor-stacking wastes up to 60% of vertical warehouse volume, restricting total plant storage capacity.
Strict FEFO & Expiration Tracking
Cocoa fats and derivative powders are sensitive to ambient temperature and expiration timelines. Guaranteeing First-Expired, First-Out (FEFO) compliance via manual pen-and-paper or basic WMS logging often causes batch mixing and costly product write-offs.
Research published in the Journal of Food Engineering highlights that maintaining constant moisture level and climate-controlled storage conditions is critical to preventing lipid crystallization and mold growth in tropical climates. Traditional forklift operations require wide aisles, creating thermal exchange channels that increase industrial refrigeration energy consumption.
How Does Automated Engineering Solve High-Density Cocoa Staging?
To overcome physical spatial boundaries and human operational delays, SSTC Intelligence engineers custom-designed automated high-bay racking systems. By transitioning static floor storage into high-density vertical infrastructure, cocoa refineries achieve total operational control while safeguarding product integrity.
Maximizing Density via Double-Deep Pallet AS/RS
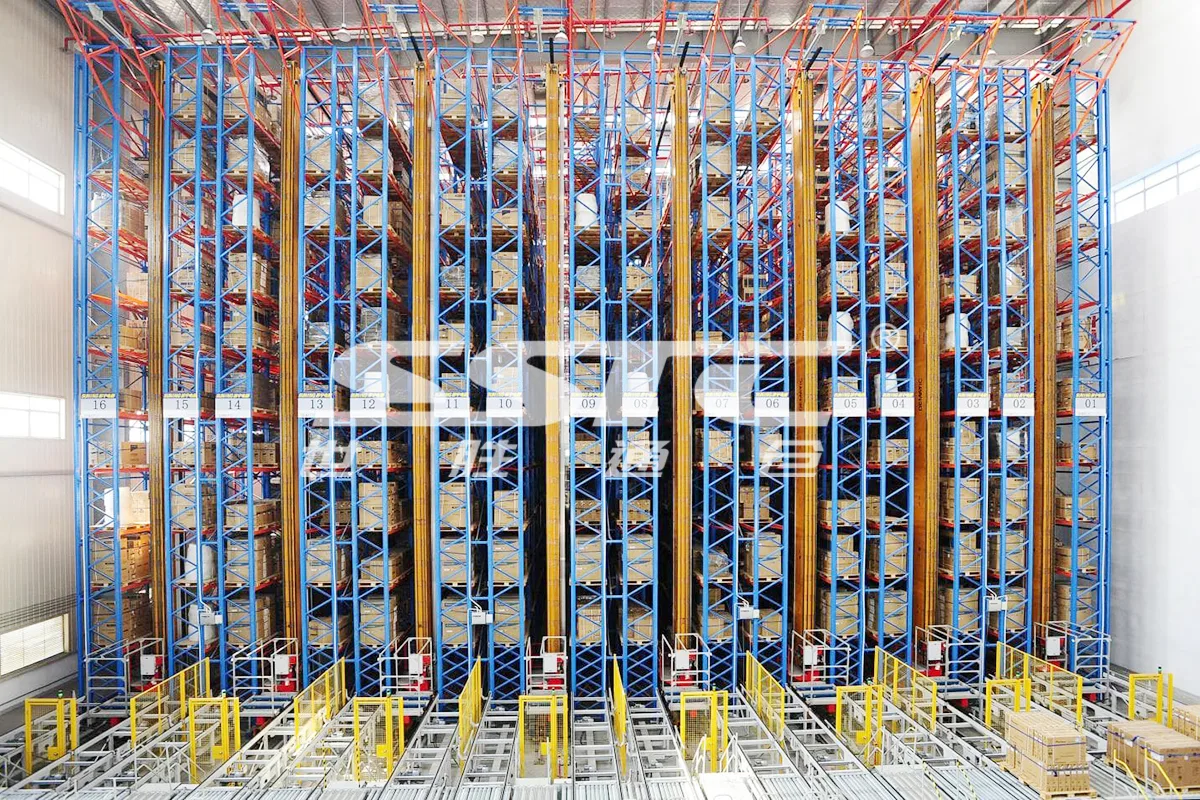
Deploying Double-Deep Pallet AS/RS allows facilities to store two pallets deep within each rack channel. This structural configuration eliminates half of the inner service aisles required in standard high-bay layouts, expanding overall storage volume by up to 40% on the exact same footprint. Heavy-duty stacker cranes handle standard cocoa pallets up to 1,500 kg reliably across heights exceeding 25 meters.
Deep-Lane Staging with Radio Shuttle Racking
For high-volume, single-SKU raw bean buffers or packaging materials, integrating Radio Shuttle Racking delivers maximum volumetric density. Semi-automated shuttles carry incoming pallets deep into storage channels, drastically cutting forklift travel times, eliminating warehouse collisions, and protecting food-grade packaging from accidental vehicle impacts.
How Does Software Orchestration Guarantee 100% FEFO Dispatch?
Hardware automation must be paired with intelligent warehouse execution logic. In cocoa derivative warehousing, software algorithms manage double-deep selectivity and automated rearrangement cycles without human intervention.
WES Dynamic Storage Allocation
SSTC Warehouse Execution System (WES) automatically evaluates incoming batch numbers, production dates, and moisture sensitivity. Pallet AS/RS stacker cranes execute background pallet rearrangement sequences during off-peak shifts, ensuring front-position pallets always match active container dispatch orders.
Seamless ERP & WMS Synchronization
Connecting physical stacker cranes directly with enterprise systems (SAP, Oracle) eliminates manual data entry errors. Every single pallet of cocoa butter or powder is tracked in real-time, providing total supply chain visibility from raw bean receiving to ocean container loading.
Performance Evaluation: Manual vs. Automated Cocoa Warehousing
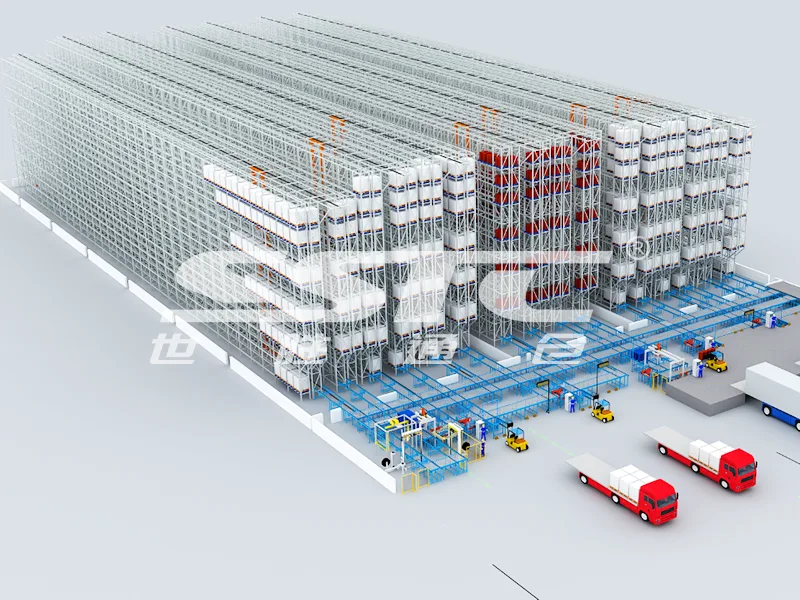
Upgrading to factory-direct automated storage yields immediate, measurable improvements across operational metrics. Below is a performance evaluation comparing traditional manual warehouse layouts with automated configurations engineered by SSTC Intelligence:
| Metric | Manual Warehousing | Pallet AS/RS Solution | Operational Impact |
|---|---|---|---|
| Storage Capacity | Standard floor stacking (3-4 levels) | High-bay vertical (up to 25m) | +180% cubic storage density |
| Dispatch Speed | 15-20 pallets per hour (Forklift) | 60+ pallets per hour per crane | 3x faster container loading |
| Inventory Accuracy | ~92% (Manual logging risk) | 99.9% Real-Time WES Tracking | Zero batch rotation errors |
| Energy Footprint | High refrigeration loss (Wide aisles) | Compact footprint (-40% volume) | Significant cooling energy savings |
Case Study & Customer Feedback: Malaysian Cocoa Refinery Project
In a recent landmark installation near Port Klang, a major international cocoa processor partnered with SSTC Intelligence to construct a high-bay finished goods staging facility. The facility required high-speed automated storage for refined cocoa butter cartons and industrial powder bags on standard 1200x1000mm pallets.
By deploying Pallet AS/RS equipped with double-deep telescopic forks and integrated conveyor transfer loops, the plant increased overall pallet capacity from 3,200 positions to over 9,000 positions without purchasing additional industrial land. Daily dispatch schedules for export containers were reduced from 8 hours to under 3 hours.
"Partnering with SSTC Intelligence transformed our downstream staging logistics. The Pallet AS/RS system delivered immediate operational stability, allowing us to manage high-volume export spikes seamlessly while maintaining 100% FEFO accuracy for our cocoa butter inventory. The build quality of the steel racking and smooth stacker crane performance exceeded our expectations."
Frequently Asked Questions About Cocoa Storage Automation
Can Pallet AS/RS handle cold-room cocoa storage?
Yes. SSTC Intelligence engineers Pallet AS/RS systems specifically for temperature-controlled and cold-room environments ranging from +5°C to +18°C. Components utilize specialized low-temperature lubricants, condensation-resistant sensors, and heavy-duty anti-corrosion structural steel coatings.
How does double-deep selectivity impact export dispatch times?
Integrated WES software schedules automatic pallet rearrangement during low-activity periods. Rear pallets needed for urgent container staging are positioned in front slots automatically, ensuring zero waiting time for outbound trucks and export staging conveyors.
Future-Proofing Southeast Asian Agribusiness Logistics
As global demand for cocoa butter, powder, and chocolate derivatives continues its steady climb across Malaysia, Asia-Pacific, and international export channels, modernizing warehouse operations is no longer optional—it is a strategic necessity. By deploying factory-direct automation solutions such as Double-Deep Pallet AS/RS, processing operators overcome acute land constraints, stabilize workforce dependencies, and achieve touchless export dispatch precision.
We Are Here to Deliver the Results You Need
Backed by our dedicated manufacturing factory, SSTC Intelligence engineers complete, factory-direct automated ecosystems. By integrating Pallet AS/RS seamlessly with warehouse management software, precision conveyors, automated stretch wrappers, and peripheral material handling equipment, we eliminate bottlenecks entirely.
Share the specific logistical challenges or floor plan constraints your facility faces today, and our expert technical team will start engineering your tailored solution.