
 AS/RS & Automatisierte Lagerlösungen | SSTC-Geheimdienst

In the realm of industrial manufacturing, few supply chains operate under margins as unforgiving as those found in the chemical and advanced new materials sectors. Whether managing volatile chemical precursors, temperature-sensitive polymers, or high-purity industrial resins, a warehouse is no longer just a passive box for inventory—it is a high-stakes ecosystem where safety, environmental compliance, and volumetric efficiency collide.
For decades, facility operators relied on conventional wide-aisle racking and manual forklift fleets to handle palletized chemical goods. Today, that legacy playbook is buckling under the weight of strict regulations, soaring real estate expenses, and the critical need for absolute zero-error handling.
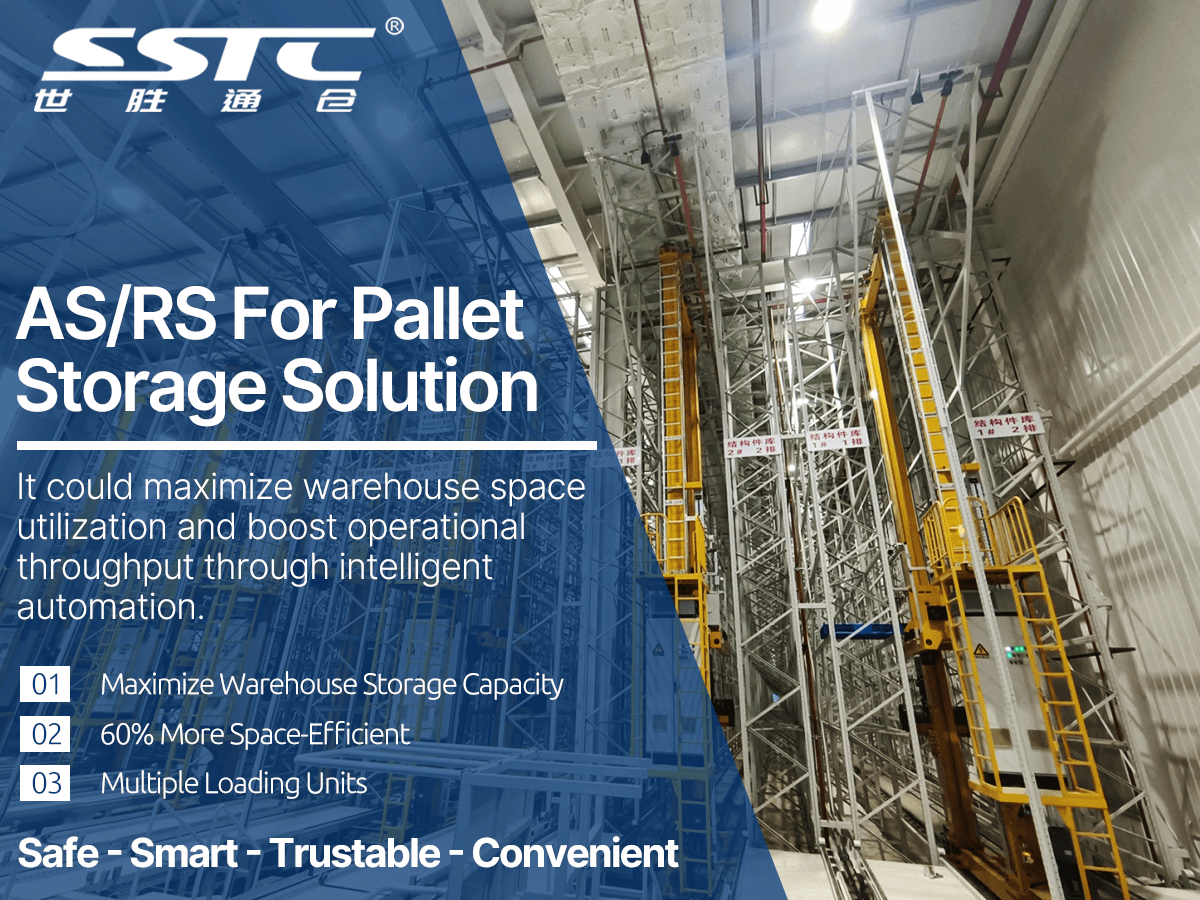
To bridge this operational gap, industry leaders are aggressively moving toward intelligent automation. At SSTC Intelligence-Technologie, our engineering teams have pioneered specialized Automated Storage and Retrieval Systems (AS/RS) designed explicitly to resolve the complex bottlenecks plaguing modern chemical and new materials distribution.
The Hidden Friction Points in Chemical Warehousing
Before evaluating solutions, we must dissect why traditional storage models fail when applied to chemical compounds and specialty materials:
The Human Safety Dilemma: Hazardous substances, corrosive liquids, and reactive agents demand minimal human exposure. Traditional manual handling places workers directly in harm’s way, where a minor forklift miscalculation can trigger catastrophic spills or structural failures. In fact, regulatory frameworks such as the OSHA Warehousing Hazards and Solutions Guide heavily emphasize that removing human operators from active storage zones is the single most effective way to eliminate workplace safety incidents.
The Imperative of Absolute Batch Traceability: Chemical manufacturing relies on strict lot numbers, expiration tracking, and flawless FIFO (First-In, First-Out) management. Manual record-keeping or fragmented warehouse management software often leads to misplaced inventory, expired raw materials, and expensive plant shutdowns.
Volumetric and Environmental Constraints: Specialized materials frequently require tightly regulated temperature, humidity, or cleanroom conditions. Wasting valuable cubic meters on wide forklift corridors means paying exorbitant operational costs to air-condition empty air.
Engineering Resilience: How SSTC AS/RS Solves the Crisis
To conquer these challenges, SSTC integrates cutting-edge hardware automation with intelligent software orchestration, offering a turnkey blueprint for modern chemical logistics.
Isolating Hazards Through High-Speed Automation
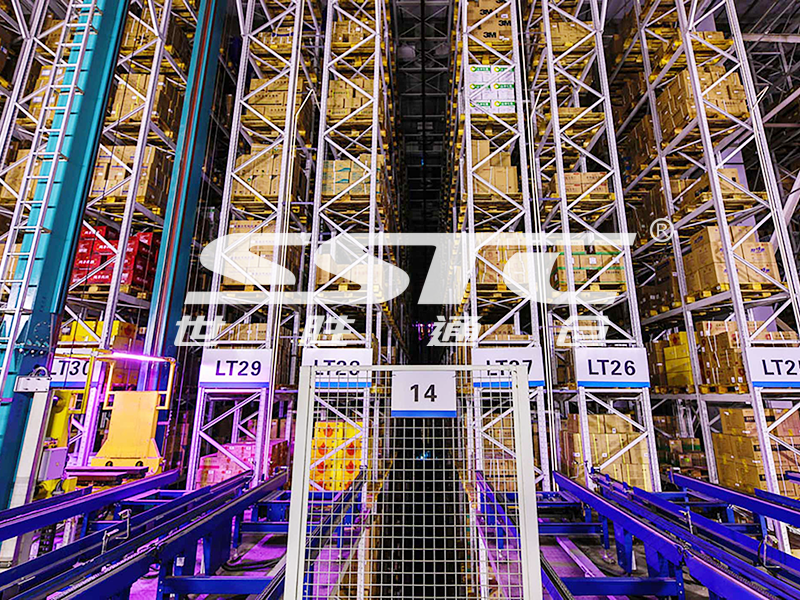
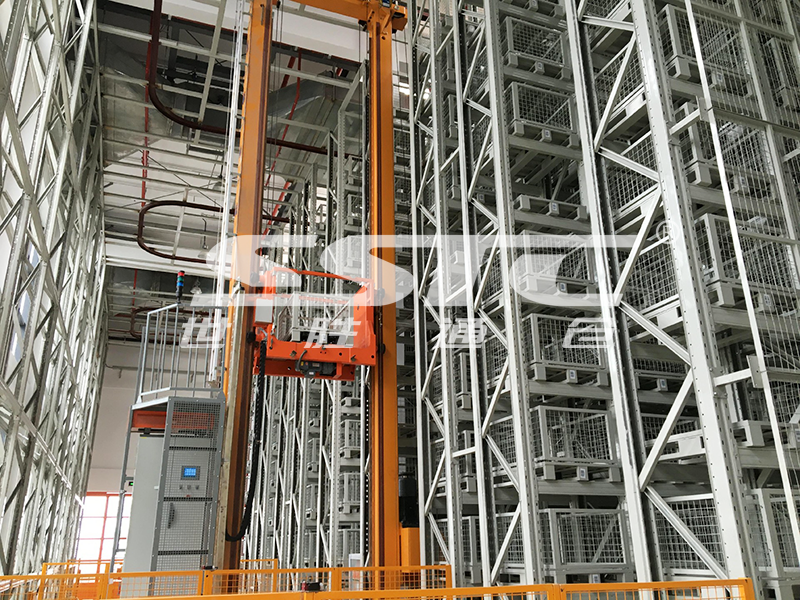
By deploying heavy-duty AS/RS stacker cranes and automated conveyor networks, SSTC systems completely remove personnel from active storage aisles. Palletized chemical loads—ranging from heavy drums to specialty resin totes—are stored and retrieved with absolute mechanical precision. This engineering approach aligns with broader industry insights highlighted in reports on Chemical Industry Automated Storage Solutions by Kardex, which stress that automated systems are vital for ensuring process reliability and secure hazardous material management.
Maximizing Cubic Space Density
Land inside modern chemical industrial parks is exceptionally scarce and expensive. SSTC high-bay AS/RS configurations scale vertically up to 24 meters or more, unlocking up to 95% cubic space utilization. This dense spatial compression significantly reduces the overall footprint that requires specialized climate control, translating directly into long-term energy savings.
Real-Time Synchronization via WMS and WCS
Hardware is only as smart as its software. SSTC’s proprietary Warehouse Control Systems (WCS) integrate smoothly with enterprise ERP platforms. Every single pallet of chemical raw materials or finished compounds is tracked in real-time, ensuring strict batch compliance, automated inventory auditing, and zero human picking errors.
Häufig gestellte Fragen (FAQ)
Q1: How do SSTC AS/RS solutions handle corrosive or hazardous chemical environments?
A: SSTC customizes its racking structures and stacker cranes with corrosion-resistant finishes, sealed electrical components, and heavy-duty structural steel designed specifically to withstand harsh chemical plant environments.
Q2: Can the AS/RS integrate with our existing plant management software?
A: Ja. Our WCS features an open-architecture design that ensures seamless data synchronization with your existing Enterprise Resource Planning (ERP) and Warehouse Management Systems (WMS).
Q3: How does automation protect against inventory damage in chemical storage?
A: By replacing manual forklift navigation with automated computer-guided machinery, the system eliminates structural collisions, drop hazards, and human mishandling errors.
Connect with Our Engineering Experts
Ready to elevate your chemical and new materials facility into a high-density, ultra-safe automated powerhouse? Talk directly to our technical consultants to explore tailored layouts for your project.
Website: www.sstc-storage.com
E-Mail: [email protected] | [email protected]
WhatsApp : +86-13671613032
SSTC Intelligence Technology — Engineering Precision, Securing Supply Chains.